
What the Plus-Minus 0.5 After Your Label Size Actually Means
The drawing says 50 by 30, plus or minus 0.5. The delivery measures 49.6 and a complaint goes out. What tolerance means, why it exists, how to measure right.
The drawing says 50 x 30 mm, followed by a plus-or-minus 0.5. The goods arrive, someone measures 49.6 with a steel ruler, and a complaint goes out: wrong size. In fact that plus-or-minus value is the tolerance, and anything between 49.5 and 50.5 qualifies as a 50 mm dimension. The real problem is that many buyers do not know why tolerance exists, or which edge to measure and how.
Tolerance Comes From the Process, Not From Laziness
Label dimensions are set by the die. Steel rule blades bent to the label outline punch the shape, and tiny offsets occur between blade position and material registration with every stroke. Flatbed die cutting typically holds around plus-or-minus 0.2 to 0.3 mm. Rotary die cutting on roll-to-roll lines does somewhat better, but the web itself stretches as it travels, and over a few hundred meters of film a half-millimeter of drift appears on its own.
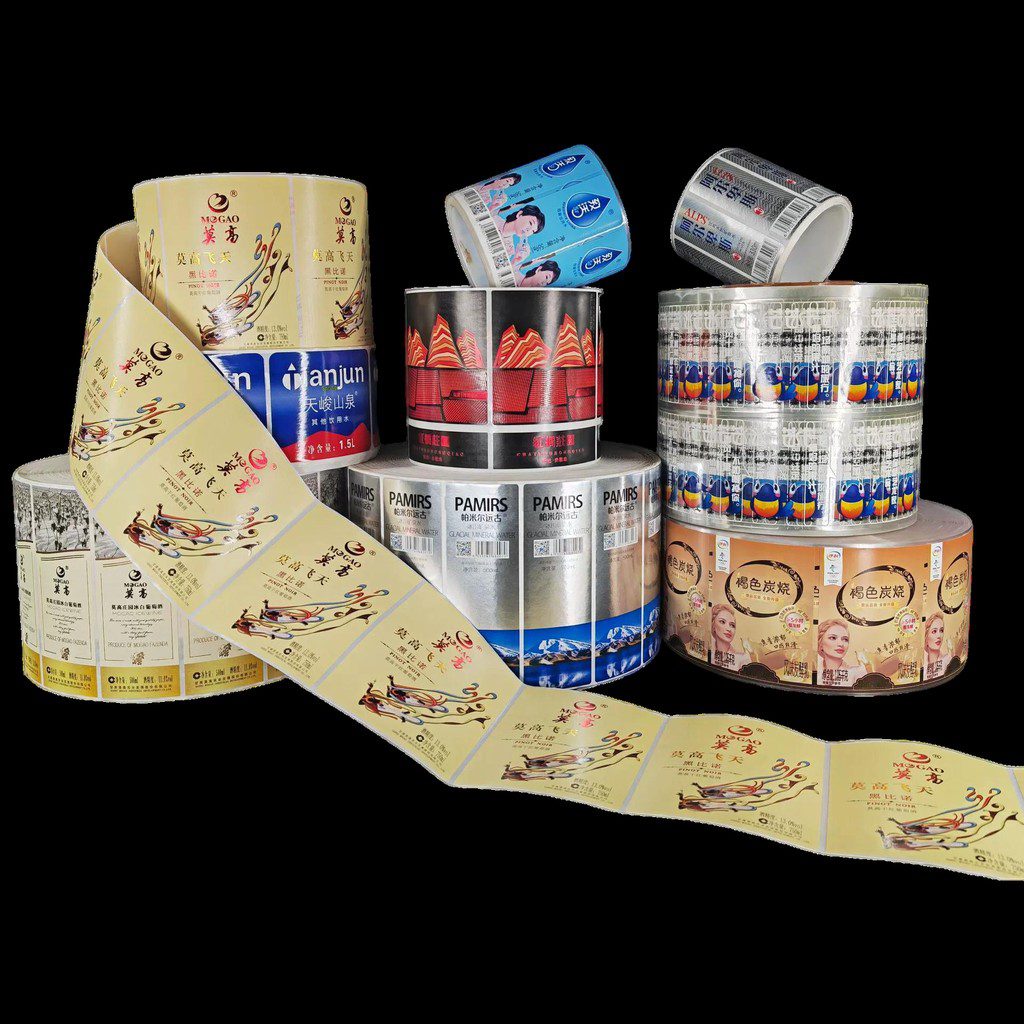
In other words, demanding that every label measure exactly 50.000 mm is demanding that machines and materials never deform. So the industry standard practice is to state a tolerance on the drawing. Plus-or-minus 0.5 mm is a normal level for rectangular labels. Odd shapes, rounded corners and narrow strips commonly carry 0.8 or even 1.0 mm. Beyond that, cost rises steeply, because tighter tolerance demands laser cutting or precision tooling.
Where to Measure
Several details trip people up when checking dimensions. First, measure the cut edge, not the printed artwork. If registration drifted slightly, the artwork sits a fraction inside the paper edge. Measuring against the artwork reports a printing offset as a cutting error. Second, measure multiple pieces. Labels are punched one after another in a continuous web. A few pieces drifting wider than the rest does not mean the whole roll is off. Proper acceptance sampling means pulling ten pieces at random, recording the maximum and minimum, and passing the batch if both fall inside the band. Third, a steel ruler cannot resolve 0.1 mm. Tolerance checks need a caliper or a measuring magnifier. Estimating to a tenth of a millimeter by eye and then disputing a plus-or-minus 0.5 specification is not a measurement at all.
Tolerance and the Machines Downstream
Tolerance is not only an acceptance clause between buyer and supplier. It directly governs the next process. Labels feeding automatic applicators or thermal printers rely on consistent edges for dispensing and sensor positioning. When a batch drifts beyond its band, applicator registration wanders and labels land crooked. A batch that cannot hold tolerance is usually not failing by that half-millimeter alone, it is failing on consistency across the entire run.
How to Specify So Nobody Loses
At Xuzhou Huaishi Electronic Technology every quotation carries a tolerance next to each dimension, both as industry practice and as protection for both sides. What buyers should do is mark the critical dimensions clearly: which edge the applicator registers against, whether there is a minimum margin requirement, whether a clear label needs print-to-cut alignment. Written into the drawing, these notes give the tolerance a concrete object. A drawing showing nothing but 50 x 30 leaves the most room for dispute.
Material matters here. Paper liners and paper face stocks take up moisture from the air and give it back, so a roll measured in a humid warehouse can differ slightly from the same roll measured in a dry, heated workshop. Film stocks stay closer to size but move with temperature. Agree on the measuring environment along with the tolerance, and let the rolls rest in the production room before checking them. Otherwise two honest measurements disagree and neither side is wrong.
And if the product genuinely is dimensionally critical, for instance the label must seat into a fixture or align with a housing opening, say so at order time. Such parts can be laser cut or precision die cut to plus-or-minus 0.1 mm, but that is a different product at a different price, and comparing it against standard die cutting is comparing two different things.